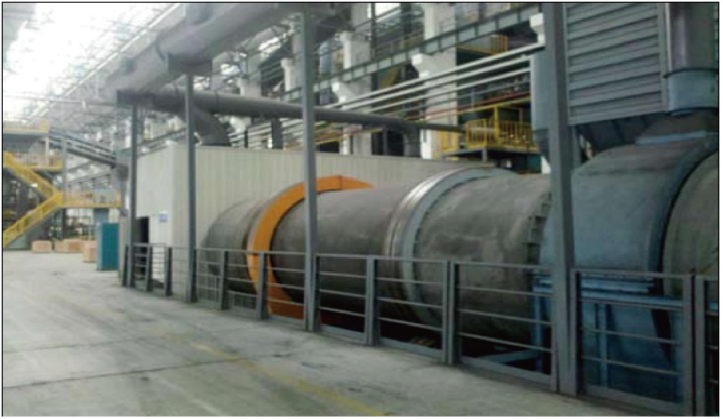
Double Layer Casting cooling cleaning
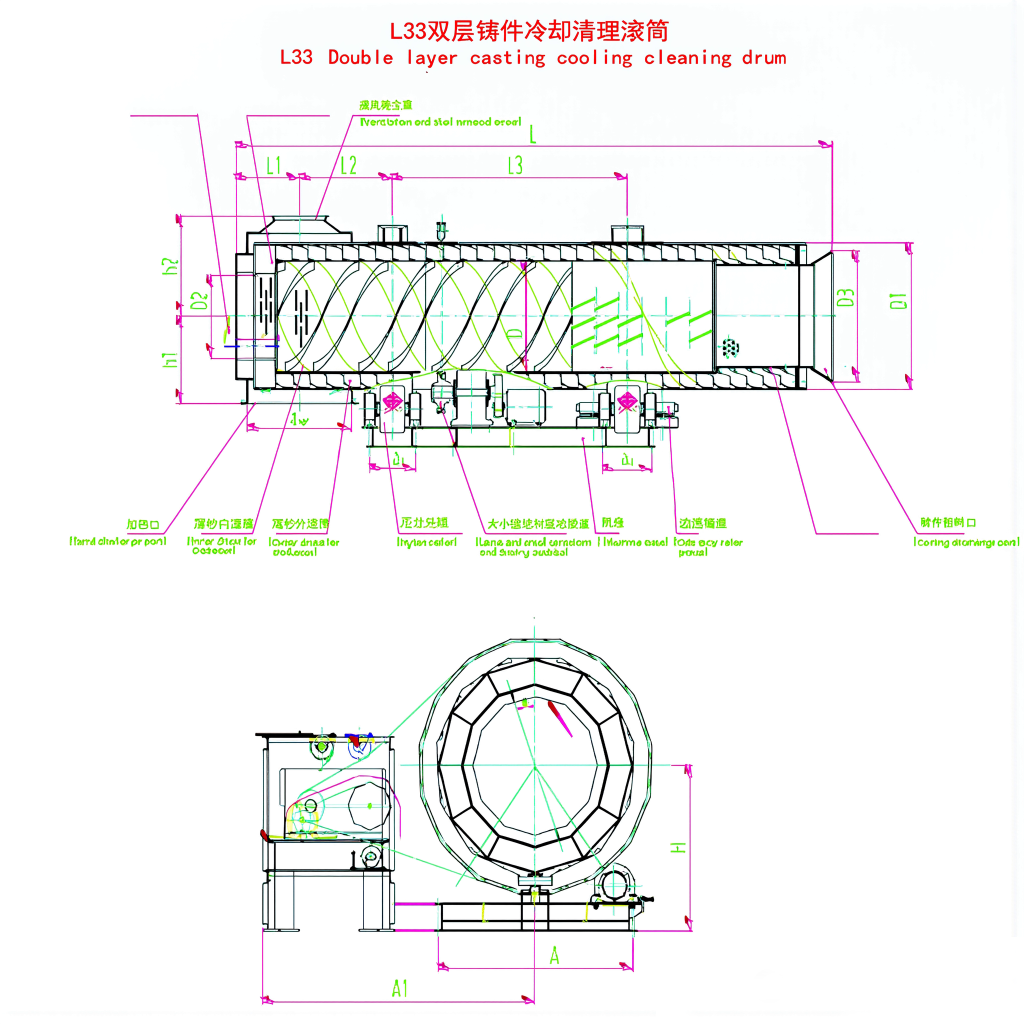
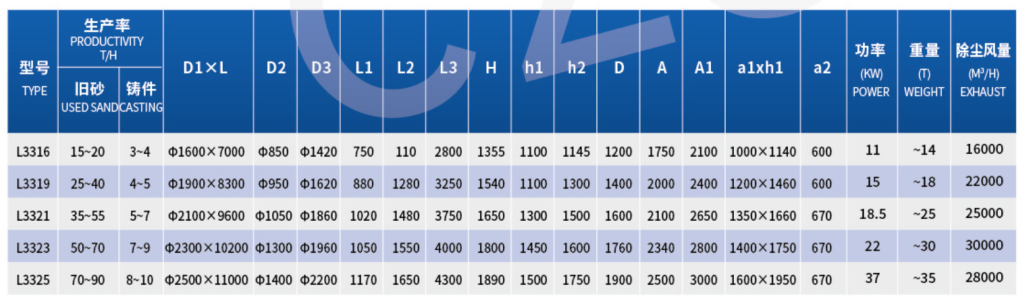
L33 Double Layer Casting cooling cleaning drum
Tons of star shaped iron blocks flow circularly in the inner and outer layer of the drum, wrap the castings in rolling which buffered the collision, protected the cleaning edge and corner, slight collision of castings, less machining allowance; Star shaped iron blocks rub and scratch repeatedly make castings smooth,no black sand stick, only small amount of white roasting bonded sand, which can avoid one clean up and deliver to shot blasting direct, which with high efficiency suitable for batch production line with high speed and high pressure for medium and small castings. The working size should be less than 1/4 ~ 1/3 of the inner diameter.
The used sand spaling from the casting, crushed and screen to the outer drum, temperature at outlet is 90~110℃, and keep ≈1.5% moisture, which creats a good condition to reduce the working of cooling and dust collect.
Lumps of used sand spaling from the hot casting crushed by star shaped iron block flow, discharged from screen gap which with wide of 16mm of the drum. The recovery rate of used sand is close to 100%.
Chain drive is used to reduce the impact of drum radial runout; the application of pouring nlon roller greatly reduced the wear of roller table.